

Press Brake Die and Punch Shipment to Zambia via Durban, South Africa
JSTMT arranged an international shipment of press brake dies and punches to Zambia in October 2026, supplying one upper punch and one multi-V lower die for sheet metal bending applications.
The shipment consisted of two pieces of press brake tooling, with a combined gross weight of 383 kg and a total volume of 0.166 CBM.
Departing from Shanghai, China, with an ETD of October 30, 2026, the cargo was routed through Durban Port, South Africa, before onward transportation to its final destination in Zambia.
This shipment demonstrates JSTMT’s capability to supply press brake punches and dies for international sheet metal fabrication customers, including destinations requiring transit through regional seaports.
Shipment Details
| Item | Details |
|---|---|
| Destination | Zambia |
| Product | Press Brake Die and Punch |
| Quantity | 2 pieces |
| Upper Tool | 1 Upper Punch |
| Lower Tool | 1 Multi-V Lower Die |
| Upper Punch Dimensions | 140 × 80 × 26 mm |
| Multi-V Lower Die Dimensions | 140 × 140 × 3218 mm |
| Gross Weight | 383 kg |
| Total Volume | 0.166 CBM |
| Departure Port | Shanghai, China |
| Transit Port | Durban, South Africa |
| ETD | October 30, 2026 |
| Final Destination | Zambia |
Press Brake Punch and Multi-V Die Included in the Shipment
This order included two different components of a press brake tooling setup: one upper punch and one multi-V lower die.
Both components work together during the bending process to form the required sheet metal profile.
1. Press Brake Upper Punch
The shipment included one upper press brake punch with dimensions of:
140 × 80 × 26 mm
A press brake upper punch is mounted on the upper beam and works with the lower die to form the required bend angle and profile.
The selection of an upper punch depends on several technical factors:
- Required bending angle
- Punch geometry and tip radius
- Material type and thickness
- Required inside bend radius
- Press brake clamping system
- Finished part dimensions
For replacement or custom punches, the machine’s tooling interface and mounting dimensions must be checked to ensure compatibility.
2. Multi-V Press Brake Lower Die
The second component was one multi-V lower press brake die, measuring:
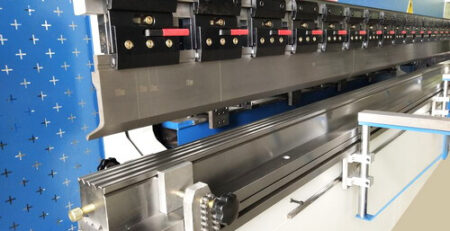
140 × 140 × 3218 mm
A multi-V die features multiple V-shaped openings in a single lower die body. This allows operators to select different V openings according to the material thickness and bending requirements.
Compared with using several separate single-V dies, a multi-V die provides greater flexibility when production involves different sheet metal thicknesses.
Key considerations when selecting a multi-V lower die include:
- Available V-opening sizes
- Material type and thickness
- Required bending angle
- Die body dimensions
- Working length
- Press brake capacity
- Tool holder and mounting configuration
The actual V-opening dimensions and allowable tooling load should be verified against the machine and material specifications.
What Is a Multi-V Press Brake Die?
A multi-V press brake die is a lower bending tool designed with several V-shaped openings in one die body.
Each V opening provides a different bending option, allowing operators to select a suitable opening for different material thicknesses and applications without changing to a separate single-V die for every operation.
Common benefits include:
- Multiple bending options: Different V openings accommodate different material thicknesses.
- Reduced tool changes: Several V openings are available in one die body.
- Production flexibility: Suitable for workshops handling different sheet metal jobs.
- Efficient tooling management: Fewer separate lower dies may be needed for a range of bending operations.
The correct V opening must still be selected according to material thickness, tensile strength, required inside radius, bending method, and machine capacity.
What Is the Difference Between a Press Brake Punch and Die?
A press brake punch and a press brake die are complementary components used together during sheet metal bending.
| Component | Function |
|---|---|
| Upper Punch | Applies the bending force to the sheet metal |
| Lower Die | Supports the material and provides the forming opening |
| Multi-V Die | Provides multiple V openings for different bending requirements |
The punch and die must be compatible with the press brake machine and the required bending application.
Their geometry, dimensions, and load capacity should be checked together to achieve consistent bending results.
How to Choose the Right Press Brake Die
Selecting the correct press brake die is important for bending accuracy, tooling life, and safe machine operation.
Before purchasing a replacement or new lower die, consider the following factors.
1. Material Type and Thickness
Mild steel, stainless steel, aluminum, and other materials have different forming characteristics. Material thickness and tensile strength influence the appropriate V opening.
2. V-Opening Size
The V opening affects the bending radius, required force, and finished-part geometry. The appropriate opening depends on material specifications and the bending method.
3. Required Bending Angle
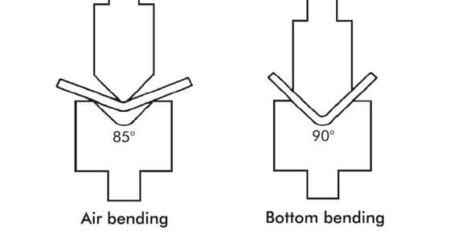
The punch angle and lower die configuration must work together to achieve the required finished angle.
4. Working Length
The die length should be compatible with the machine and the workpiece dimensions.
5. Machine Compatibility and Load Capacity
Check the tooling mounting system, machine capacity, and allowable tooling load before installation.
For custom press brake dies, supplying a drawing, machine information, or existing tooling dimensions helps verify the required configuration.
For additional information, see our press brake punch and die solutions and press brake tooling selection guide.
Shipping Press Brake Dies to Zambia via Durban Port
Zambia is a landlocked country without direct access to the sea. International cargo shipments to Zambia can therefore involve transportation through seaports in neighboring countries.
For this order, JSTMT arranged the following transportation route:
Shanghai, China → Durban Port, South Africa → Zambia
The shipment had an estimated time of departure (ETD) of October 30, 2026, from Shanghai.
Durban Port served as the intermediate maritime port before the cargo continued by onward transportation toward Zambia.
The shipment consisted of two pieces of relatively heavy press brake tooling, with a combined gross weight of 383 kg and a volume of 0.166 CBM.
For international tooling orders, transportation arrangements are selected according to the destination, cargo dimensions, weight, and delivery requirements.
JSTMT Press Brake Punch and Die Supply
JSTMT manufactures and supplies press brake punches, lower dies, and custom bending tools for industrial sheet metal fabrication.
Our press brake die and punch range includes:
- Standard Press Brake Punches
- Acute Punches
- Gooseneck Punches
- Heavy-Duty Punches
- Radius Punches
- Standard V Dies
- Multi-V Dies
- Hemming Dies
- Offset Dies
- Custom Punches and Dies
Tooling can be supplied in different configurations to suit compatible press brake systems and customer bending applications.
For non-standard requirements, customers can provide drawings, samples, machine details, or existing tooling dimensions for technical review.
Request a Press Brake Die and Punch Quote
Looking for a press brake die, multi-V lower die, or replacement upper punch?
Send JSTMT the following information for a quotation:
- Press brake brand and model
- Required punch or die type
- Tooling dimensions
- V-opening specifications, if applicable
- Material type and thickness
- Required bending angle
- Tooling drawing or sample
Our team can review your specifications and provide a quotation for suitable standard or custom press brake punches and dies.
Contact JSTMT for your press brake tooling requirements.




Leave a Reply